
- 2
- 3
- 4

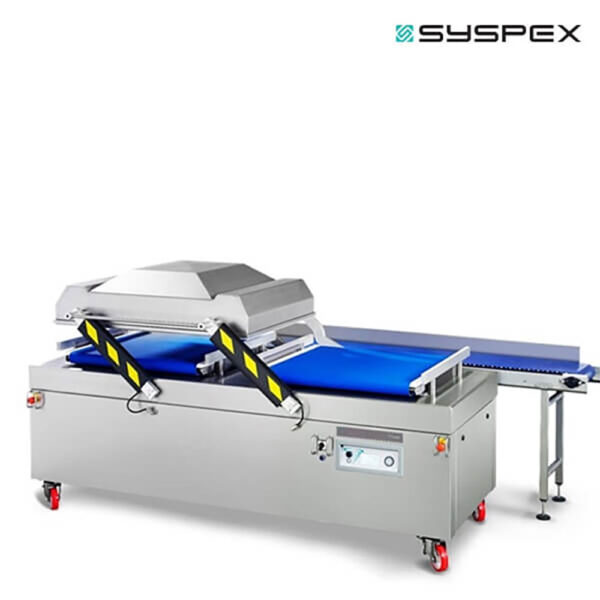


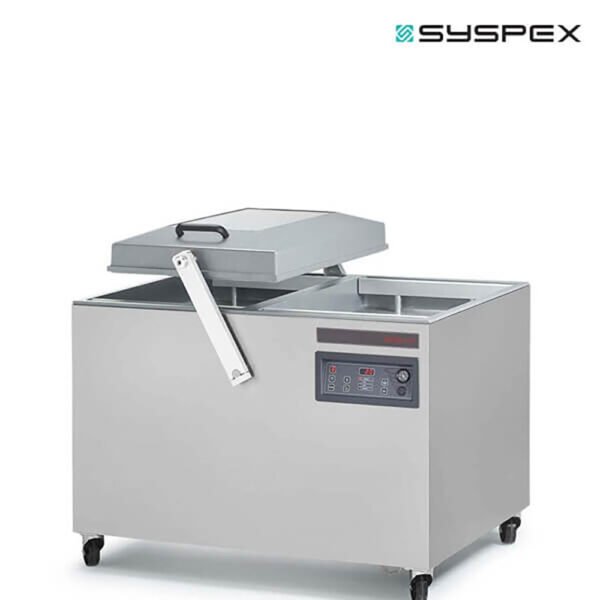
Extended Product Freshness and Severe Oxygen Reduction
Perishable foods, proteins, cheeses, and delicate electronic components require absolute isolation from atmospheric moisture and oxygen to prevent degradation. Sourced industrial vacuum sealing systems utilize heavy-duty vacuum extraction cycles to pull 99.9% of the air out of the packaging pocket before executing a high-integrity thermal seal. This complete evacuation halts the growth of aerobic bacteria, prevents freezer burn on frozen foods, and locks in original product freshness, flavors, and weight without relying on chemical additives.
High-Speed Packaging Adaptability for Diverse Substrates
Manual bag clipping and unoptimized sealing bars create structural packaging bottlenecks and lead to premature seal failures during transport. As an end-to-end solutions provider, Syspex resolves these floor challenges by sourcing industrial vacuum chambers and continuous vacuum sealers engineered for heavy-duty cycle speeds. These rugged systems easily accommodate multiple bag thicknesses, flexible barrier pouches, and aluminum co-extruded films, providing a perfectly flat, leak-proof hermetic closure that secures bulk ingredients, consumer-ready portions, and industrial components cleanly.
The SYSPEX Advantage in End-to-End Integration
- 30 Over Years of Industrial Experience With over three decades of work, we act as your trusted solutions provider. We deliver complete packaging line risk audits, pouch material selection, and throughput optimization consultation.
- Consultative Engineering We work closely with your team to review your specific product moisture levels, package dimensions, and hourly production targets, ensuring your sourced vacuum equipment is configured perfectly.
- Regional In-House Technical Expertise Our own technical engineer team is located in Singapore, Malaysia, and Indonesia. This means we can provide rapid system installation, seal bar temperature calibration, and regular vacuum pump maintenance support.
- Sustainability Commitment We supply energy-efficient vacuum machinery equipped with smart eco-mode functions and high-yield pump cycles that minimize electrical draw while reducing total plastic film thickness requirements.
Frequently Asked Questions
Vacuum packaging removes oxygen from inside the protective pouch or bag, which effectively starves aerobic bacteria and molds that cause food spoilage. By neutralizing the oxidation process, fresh food shelf life is typically extended by three to five times compared to traditional storage methods, preserving color, texture, and taste during transport.
Depending on your specific processing volumes, we supply single-chamber vacuum sealers, heavy-duty double-chamber systems for continuous alternating operations, and automated belt-fed external vacuum sealers designed for high-throughput automated packing lines.
Yes. Sourced industrial chamber vacuum sealers are engineered to handle high-moisture foods, sauces, and liquids effortlessly. By balancing the atmospheric pressure inside the entire chamber during the extraction cycle, liquids remain securely inside the bag rather than being drawn into the vacuum pump network.
To prevent slow air ingress over time, vacuum sealing requires high-performance co-extruded barrier pouches (typically PA/PE combinations). We supply a broad range of high-barrier food packaging consumables that provide excellent puncture resistance and reliable seal stability under deep vacuum pressure.
Absolutely. Sourced chamber units can be optioned with gas-injection kits for Modified Atmosphere Packaging (MAP). This allows the machine to pull a full vacuum and then inject a precise mixture of food-grade gases (such as nitrogen or carbon dioxide) to protect fragile items from crushing while maintaining freshness.
The return on investment is driven by a massive reduction in product inventory waste, zeroed-out spoilage returns from retailers, and significantly lower labor hours through rapid cycle automation. Upgrading your vacuum sealing setup preserves structural quality while optimizing long-term production overhead.